English
PTFE Thread Seal Tape
Home / Product / PTFE Thread Seal Tape / Black PTFE Thread Seal Tape for Chemical and Pharmaceutical Applications
 James@eternalfriendship.net
 +86-13516706146
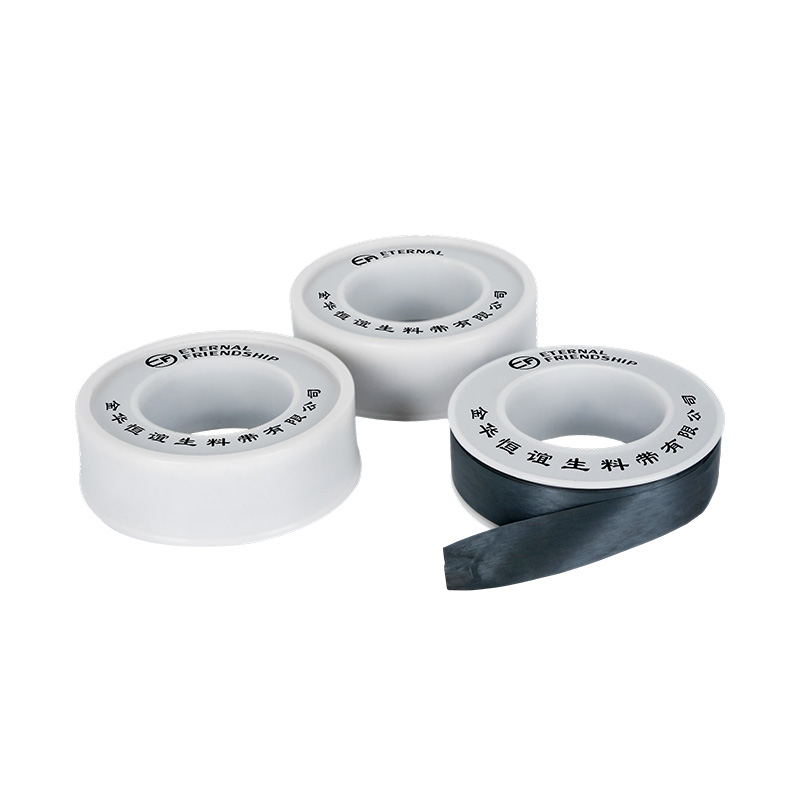
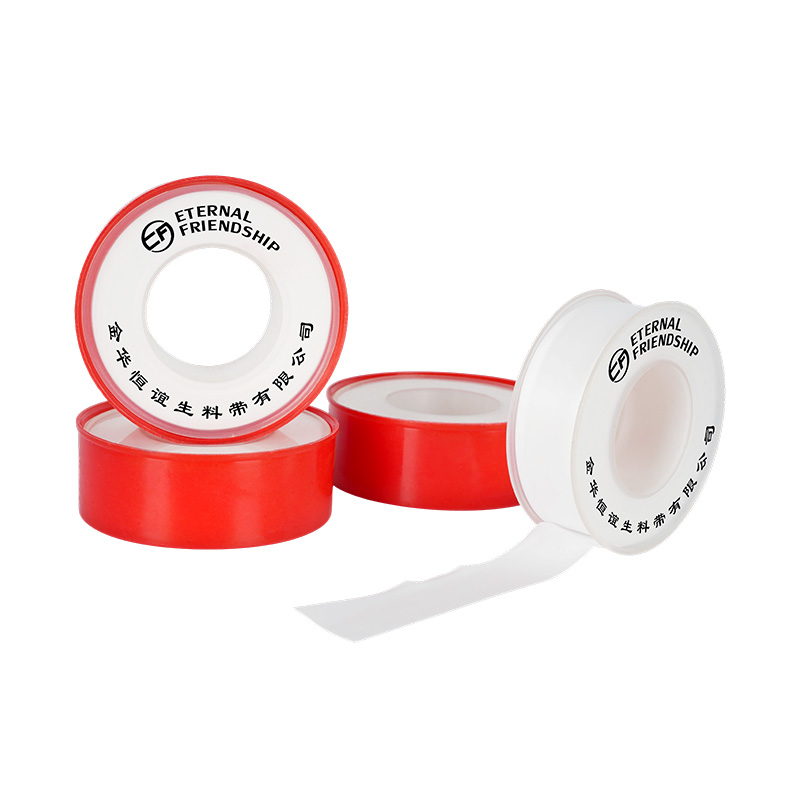
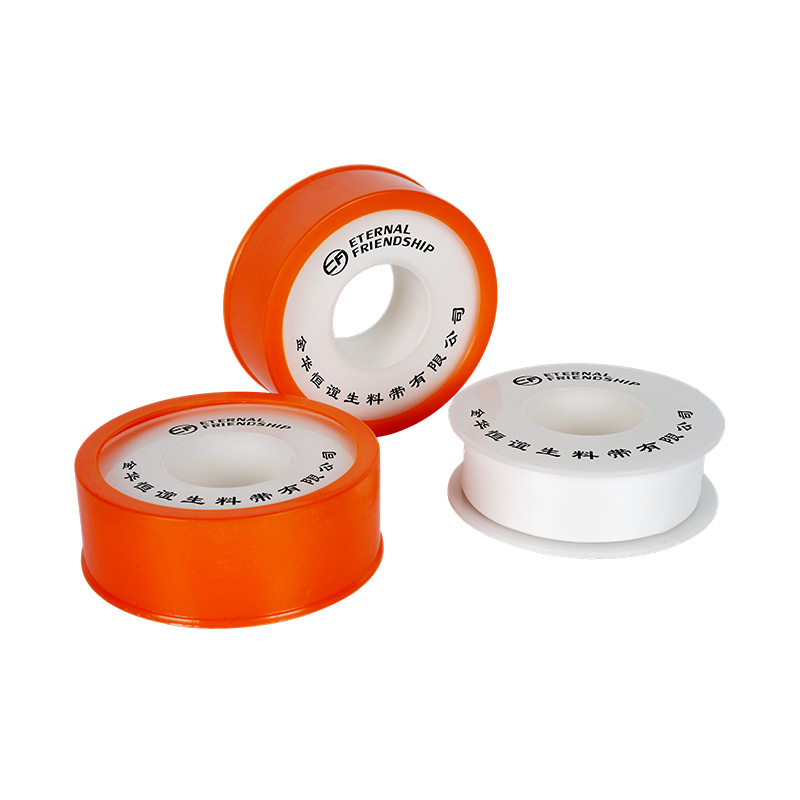
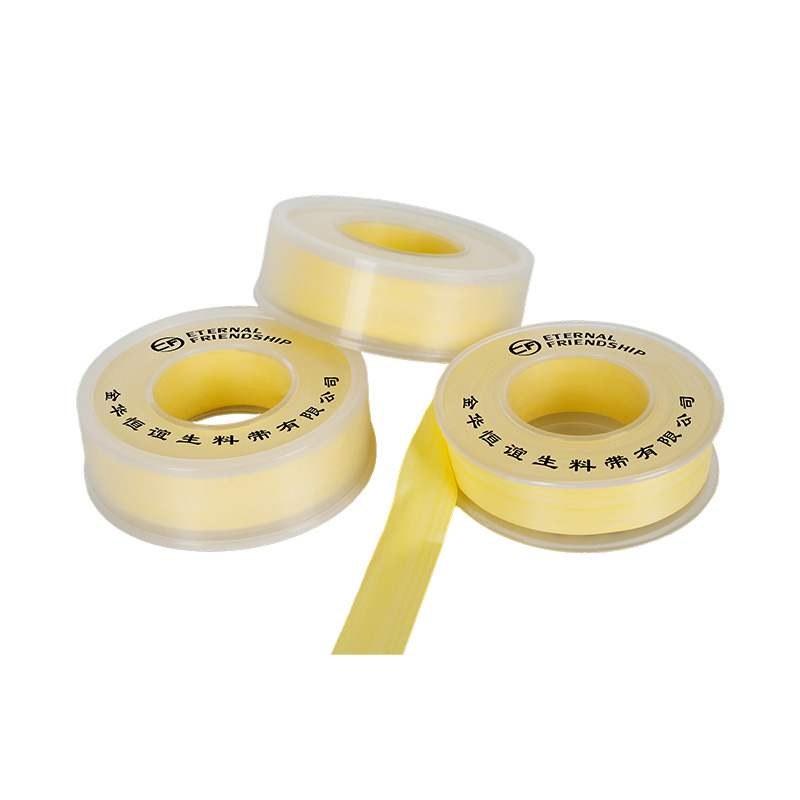
Black PTFE sealing tape (specifically, oil-impregnated black PTFE braided packing or sealing tape) is widely used in sectors such as the chemical and pharmaceutical industries, where requirements for sealing integrity and cleanliness are extremely high. Based on its material properties and typical industrial operating conditions, this type of black sealing tape offers the following key features:
1. Excellent Chemical Resistance and Media Compatibility
Chemical and pharmaceutical production often involves complex fluid media. Black PTFE sealing tape inherits the outstanding chemical stability of PTFE; with the exception of strong oxidizing agents, it withstands corrosion from the vast majority of chemical reagents. This makes it an ideal sealing choice for agitators, mixers, and centrifugal pumps handling various solvents, acids, and alkalis.
2. Superior Thermal Conductivity and Tear Strength
Unlike standard white PTFE, black sealing tape is typically braided from PTFE fibers containing graphite particles and is oil-impregnated. The addition of graphite provides high thermal conductivity, allowing it to better handle temperature fluctuations in chemical reactors or pipelines. Simultaneously, this structure imparts high tear strength and wear resistance, ensuring long-lasting sealing stability.
3. Low Friction Coefficient and Durable Self-Lubrication
The oil-impregnated black sealing tape features a very low coefficient of friction and excellent self-lubricating properties. During high-speed pump shaft rotation or frequent valve operation, it effectively reduces mechanical wear and prevents seizing, thereby significantly extending the service life of equipment components.
4. Compliance with Pharmaceutical-Grade Hygiene and Contamination-Free Standards
The pharmaceutical industry imposes strict requirements regarding material non-toxicity and non-migration. High-quality black PTFE sealing tape is made of pure, non-toxic, and odorless material that does not leach harmful substances into pharmaceuticals or food products. It is specifically recommended for clean operations in the pharmaceutical, fine chemical, and food industries where contamination must be strictly avoided.
5. Wide Operating Temperature and Pressure Range
Chemical production environments often involve extreme operating conditions. This type of black raw material tape maintains stable performance across a wide temperature range (typically withstanding high temperatures of up to 260°C–280°C) and possesses exceptional pressure-bearing capabilities, meeting the sealing requirements of various equipment such as rotary pumps, reciprocating pumps, and high-pressure valves.
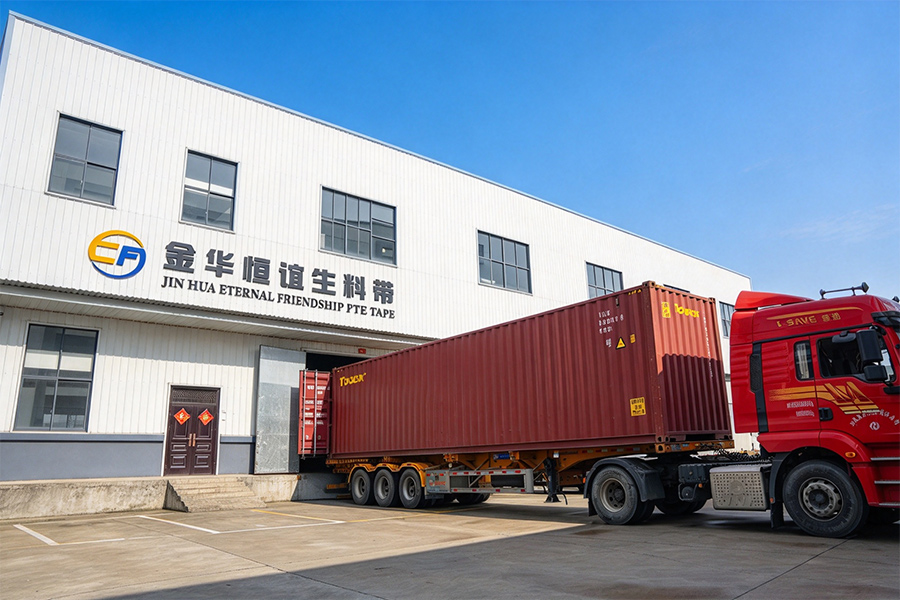
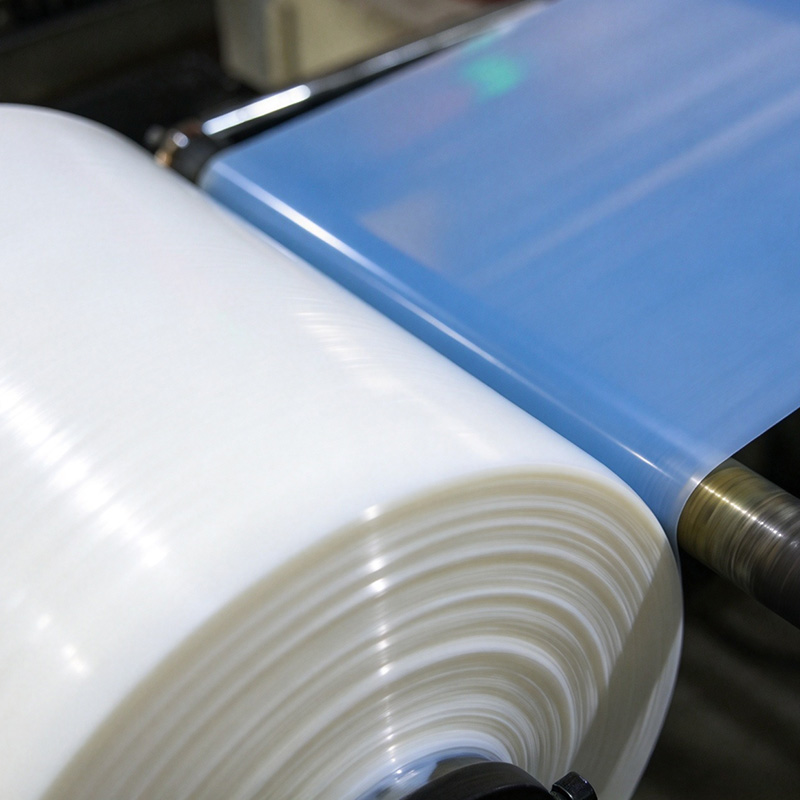
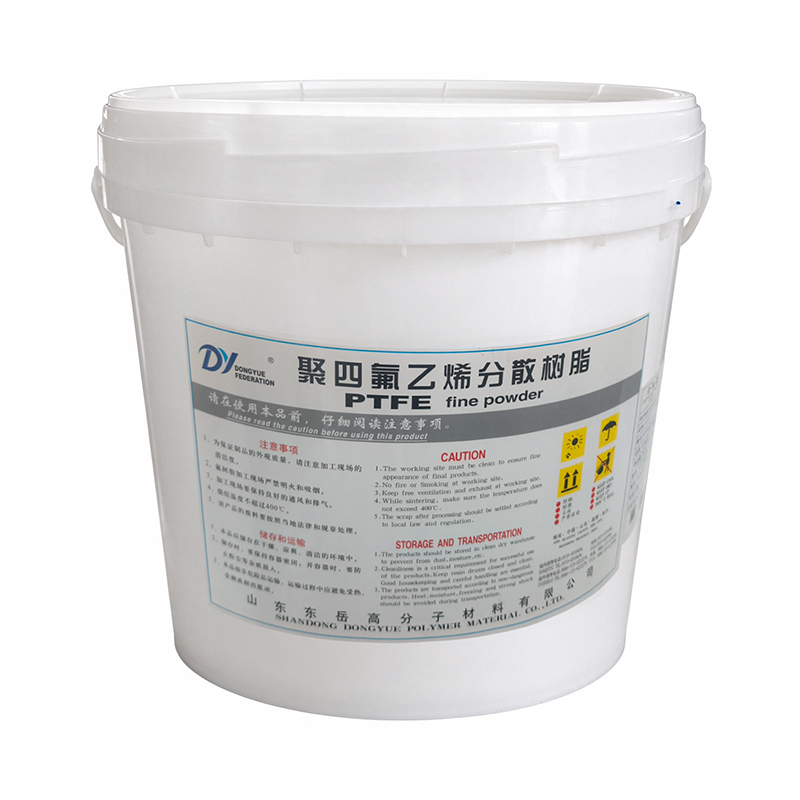
Founded in 2014, Eternal Friendship specializes in the R&D, production and supply of PTFE sealing products and corresponding supporting solutions. Over the years, the company has built a solid foothold in the PTFE thread seal tape sector, and gradually expanded its business scope to PTFE raw materials, manufacturing equipment and industrial application solutions, amassing extensive industry expertise throughout its development.
With consistent product quality, a competitive pricing structure and professional, efficient service capabilities, we continuously deliver reliable sealing product solutions to customers worldwide.
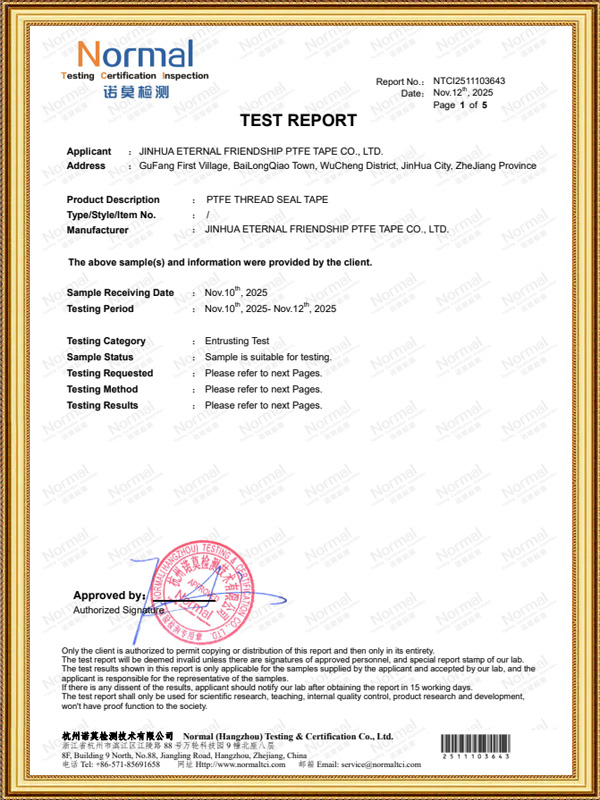
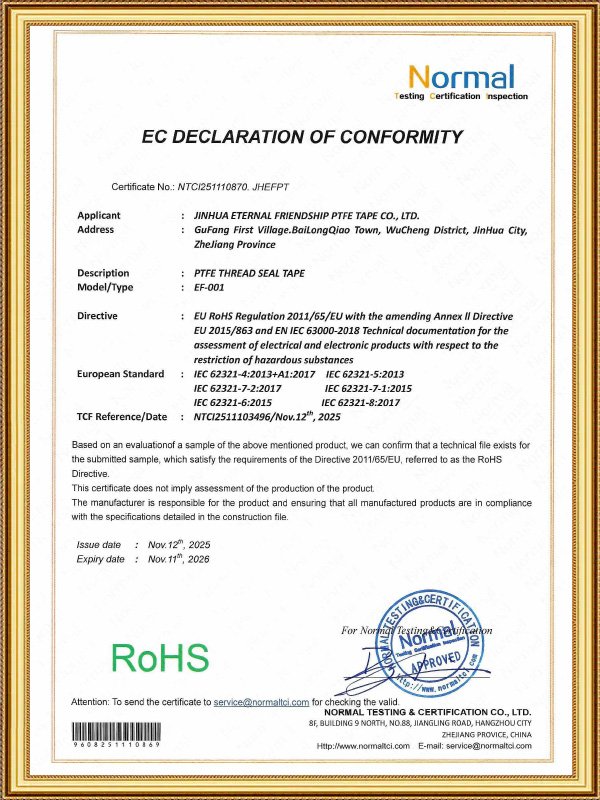
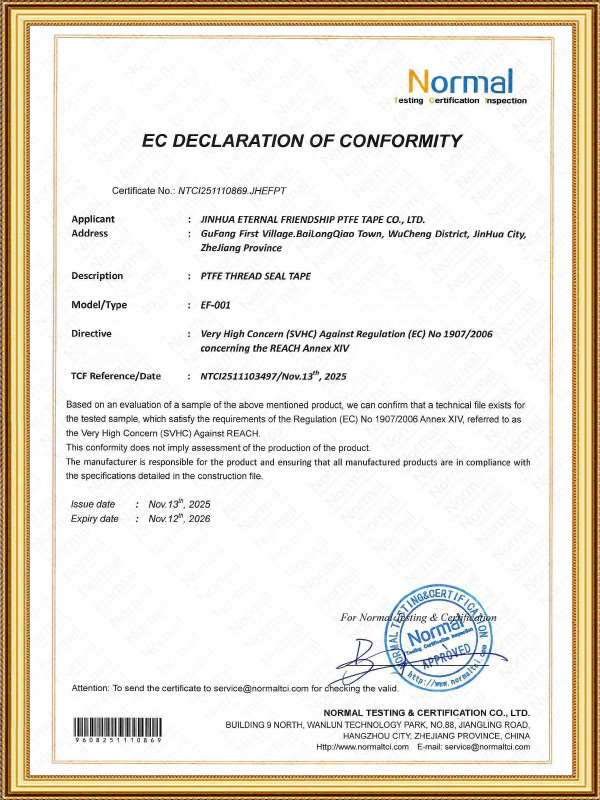
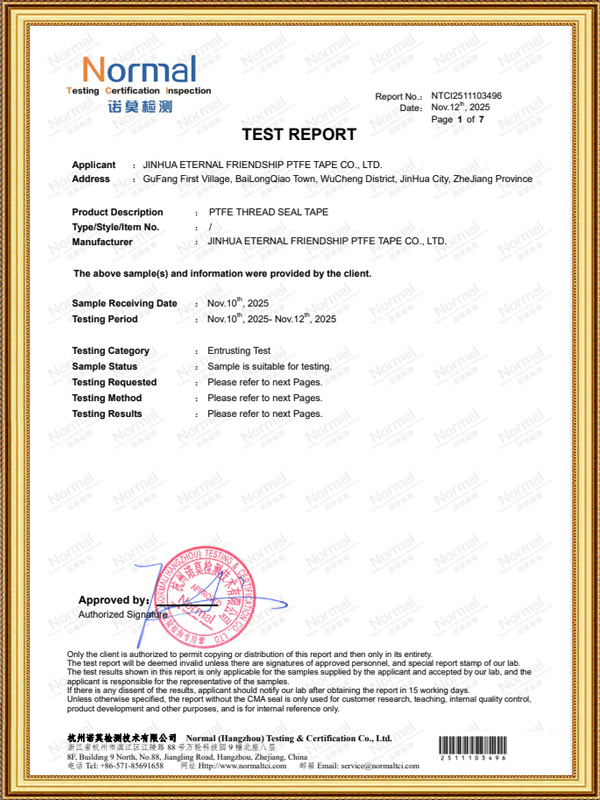
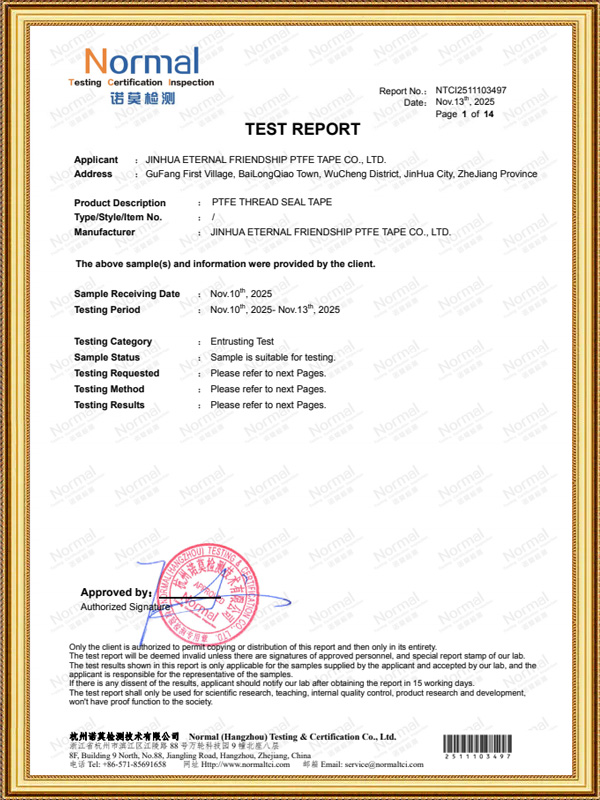
PTFE thread seal tapes all bear the same name, yet their quality varies widely across the market. Many customers encounter issues such as easy breakage, uneven thickness and sealing failure after rece...
READ MOREMany purchasers are prone to pitfalls during product selection: one type of PTFE tape cannot fit all pipeline scenarios, and selecting the wrong specification may lead to leakage, breakage and other i...
READ MOREPTFE, short for Polytetrafluoroethylene, has become the preferred material for pipe thread sealing thanks to its unique material properties. Many purchasing customers wonder what the core advantages o...
READ MORE
Mobile
Contact Us Now
Please contact us and look forward to happy cooperation with you.
Quick Link
Product Center
Contact Details
Tel: +86-0579-82111234
Phone +86-13516706146
Email: James@eternalfriendship.net
Add: Bailongqiao Town, Wucheng District, Jinhua City, Zhejiang Province, China